If you’re reading this, chances are you’re either a manufacturing engineer, a procurement manager, or a quality control lead working with investment casting machining parts — and let’s be real, misstoring these components can turn a perfectly good, precision-machined part into scrap faster than a machine tool can trigger a tool change. I’ve been in the investment casting machining supply business for 12 years, working with aerospace, medical device, and automotive clients who rely on parts with tolerances measured in ten-thousandths of an inch. Over that time, I’ve seen everything from rust on stainless steel fittings to warped titanium brackets because of improper storage. Today, I want to pull back the curtain on the storage best practices we’ve tested, refined, and lived by to keep our parts (and our clients’ production lines) running smoothly. Investment Casting Machining
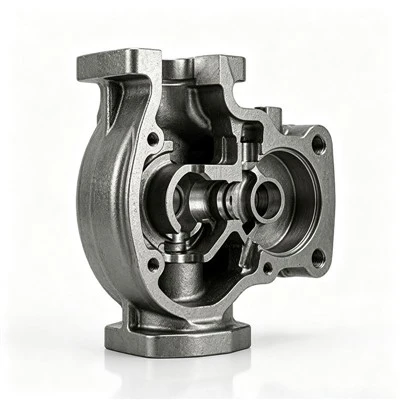
First, let’s ground this in what investment casting machining parts actually are. The investment casting process uses a wax pattern, a ceramic shell, and molten metal, then we machine the final component to tight tolerances. Unlike stamped or forged parts, these are near-net-shape — the machining step is where we dial in exact dimensions, surface finishes, and feature details. That means two things for storage: first, the parts have delicate machined surfaces that can scratch, dent, or corrode if handled wrong, and second, their precision tolerances mean even minor warping from improper stacking or moisture exposure can make them unfit for assembly.
Let’s start with the foundation: storage environment. Too many facilities toss parts on a shop floor pallet and call it a day, but even controlled-temperature warehouses can have hidden issues. We measure our storage spaces’ relative humidity (RH) weekly — and for most metal investment casting parts, the sweet spot is 30% to 50% RH. Why? Below 30%, some metals, especially aluminum and certain stainless steels, can develop “white rust” or static-induced surface defects that are impossible to machine away without ruining the part. Above 50%, moisture accelerates corrosion: even a thin layer of oxidation on a medical-grade titanium hip component can compromise biocompatibility, while carbon steel parts can start rusting in as little as 72 hours if left uncovered. We also keep storage spaces between 60°F and 75°F (15°C to 24°C) — extreme temperatures cause thermal expansion, and if parts are stored at a different temp than their assembly line, they’ll change dimensions once they’re moved, throwing off fit.
Next, part separation and organization. A common mistake our clients make is mixing different part types in the same bin. For example, a machined brass electrical connector has a soft surface that can scratch a harder, aerospace-grade Inconel turbine blade stored above it. Worse, dissimilar metals in close contact (especially in high-humidity areas) trigger galvanic corrosion — a chemical reaction where one metal leaches ions into the other, pitting surfaces deep enough to fail inspection. We use two rules here: first, group parts by material (stainless steel, titanium, aluminum, brass) and by hardness, with harder parts on lower shelves and softer parts on upper levels, so any minor shifting won’t cause contact damage. Second, separate parts by size and feature: we set aside dedicated bins for parts with delicate threads, like fasteners, so their threads don’t get cross-threaded or loaded with debris. We also label every bin with a unique part number, tolerance range, and delivery date — no more digging through unlabeled piles looking for a specific bracket that meets a ±0.001 inch dimension. That’s not just about organization; it’s about traceability, which is non-negotiable for regulated industries like medical and aerospace.
Then there’s handling and packaging, two steps that go hand in hand with storage. When a part leaves our machining facility, it’s just come off a CNC machine, with metal chips and cutting fluids still on it — so the first rule is: never store a part before cleaning it. We use a two-step cleaning process for all our parts: first, a solvent wash to remove residual cutting fluids, then a deionized water rinse, followed by a forced-air dry (we don’t let parts air-dry, which leaves water spots). Any leftover debris not only causes corrosion but also can get trapped in machined features during storage, leading to assembly issues later. For packaging, we don’t use generic cardboard boxes. For most non-critical parts, we use static-dissipative poly bins with dividers, so parts don’t rub against each other. For high-precision or delicate parts, like medical implant components, we use custom-fit foam inserts (we machine the foam to match the exact part shape) so there’s zero movement in the bin. We also wrap parts in moisture-vapor barrier (MVF) film before sealing them in bins — this is key for long-term storage (over 30 days). Regular plastic wrap isn’t enough; it traps moisture. MVF film blocks moisture vapor, so even if a storage space’s RH fluctuates, the part stays dry inside the sealed package. For parts with threaded holes or small features, we cap those holes with plastic plugs before packaging — this keeps dust and debris out, which is a silent killer. I’ve seen a $5,000 aircraft bracket rejected because a tiny metal chip got stuck in a bolt hole during storage, and the inspection team couldn’t clear it without damaging the part’s threads.
Warping prevention is another big one, especially for thin-wall investment casting parts. These are parts with walls thinner than 0.125 inches, like exhaust manifolds or turbine blades. If you stack them flat on top of each other, the weight of upper parts compresses the lower ones, causing permanent warping — even if the metal is strong. We solved this by using custom storage racks that support thin-wall parts along their natural structural points. For example, a turbine blade’s airfoil has two edges that take up the most stress, so we hang them vertically from these edges, spacing each blade 1 inch apart so they don’t touch. For flat thin-wall parts, we use edge-stacking racks instead of horizontal pallets — leaning them at a 15-degree angle distributes weight evenly, so no part bows. We also never store thin-wall parts for more than 90 days without rotating them — rotating every 30 days prevents any residual stress from setting in one position, which reduces warping over time. This might sound like extra work, but it’s way cheaper than scrapping a batch of thin-wall parts that warped in storage.
Security and inventory rotation wrap up the best practices. Investment casting machining parts are often high-value, especially for aerospace or medical applications, so we restrict access to our storage areas to authorized personnel only — no unauthorized touching or moving of parts. We also follow the FIFO (First In, First Out) inventory method: parts that arrive in storage first get used first, regardless of size or tolerance. This is critical because even with proper storage, metal parts degrade slightly over time — oxidation can form a thin layer, and if a part is stored for 6 months, that layer is thicker than it would be after 1 month, and may require extra polishing (which can alter tolerances). We track inventory with a digital system, so we can see exactly when each part was stored, and prioritize older parts for delivery. We also do quarterly visual inspections of stored parts: check for rust, oxidation, surface scratches, or warping, and if any part shows signs of damage, we set it aside for re-inspection or re-machining instead of letting it go to a client.
Now, I know what some of you might be thinking: “These practices are great for your shop, but do they translate to my facility?” The short answer is yes, and we’ve helped dozens of clients implement these steps, cutting their part rejection rates from 8% to less than 1% in some cases. If you’re struggling with part failures from storage-related issues, start small: test the humidity level in your storage space, clean parts before storage, and separate soft and hard materials. Once you see the difference, you can expand to custom racks and FIFO inventory.
At the end of the day, storing investment casting machining parts isn’t just about keeping them organized — it’s about protecting the precision and quality that went into machining them. A part that’s perfect off the CNC machine can be ruined in storage, and that’s a loss for both you and your clients. If you’re currently dealing with inconsistent part quality from storage, or you need to learn more about how we package and store parts for long-term or just-in-time delivery, feel free to reach out to discuss your specific needs.
Steel Casting Machining References:
- ASM International. "Metals Handbook: Volume 4: Heat Treating." 10th Edition, ASM International, 2018.
- Investment Casting Institute. "Best Practices for Post-Casting Handling and Storage." Investment Casting Institute, 2021.
- Aerospace Materials Specification (AMS) 2750: "Pyrometry, Heat Treatment of Aerospace Materials." SAE International, 2022.
- ISO 9001:2015. "Quality Management Systems — Requirements." International Organization for Standardization, 2015.
Ningbo Yirui Machinery Manufacturing Co., Ltd.
As one of the most professional investment casting machining manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to wholesale durable investment casting machining made in China here from our factory. Customized orders are welcome.
Address: No.107, Wanzhong Village, Jishigang Town, Haishu District, Ningbo City
E-mail: James.he@yiruitek.com
WebSite: https://www.yiruime.com/
