As a weld end cap supplier with over 15 years in the industrial piping component space, I’ve seen firsthand how even the smallest misstep in welding a pipe to an end cap can derail an entire project. I recently got a call from a pipeline maintenance manager who’d had to replace 12 end caps on a natural gas line in the Midwest—all because the weld failed prematurely. When I dug into the issue, he told me his team had skipped the step of matching end cap material to pipe, and they’d rushed the pre-weld surface prep. That’s the kind of avoidable mistake that costs time, money, and even safety. Today, I’m breaking down exactly what my team teaches every client: how to ensure a good, long-lasting weld between your pipe and our weld end caps. Weld End Caps
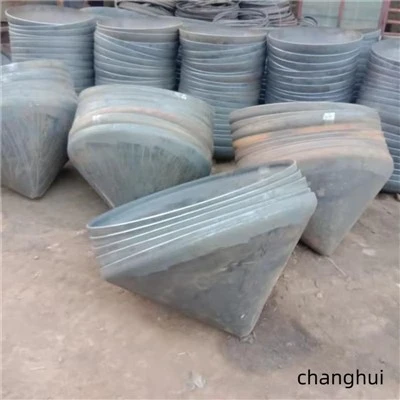
First, let’s start with the foundation: material compatibility. This is non-negotiable, and it’s the reason we always ask clients to send us a sample of their pipe before we manufacture end caps for them. Too often, people treat end caps as one-size-fits-all, but that’s a myth. Welding is a metallurgical process, and if your end cap’s material doesn’t match the pipe’s, you’re setting yourself up for failure. For example, if you’re working with carbon steel pipe, you can’t use a stainless steel end cap unless you’ve accounted for the galvanic corrosion that will occur at the weld joint over time. Even a 10% difference in material composition, like using a low-carbon steel pipe with a high-carbon steel end cap, can lead to hardening in the weld zone, making it brittle and prone to cracking under pressure or temperature fluctuations.
I remember a client in the oil and gas sector who tried to cut costs by ordering a generic carbon steel end cap for their 316 stainless steel pipe. Within 6 months, the weld corroded through, causing a leak that shut down their rig for 3 days. They came back to us afterward, and now we include a material compatibility checklist in every end cap order to prevent that from happening. The key here is to confirm three things: the base metal type (carbon steel, stainless steel, alloy steel, etc.), the material grade (like A53 for pipe, A105 for carbon steel end caps, or 304L for low-carbon stainless), and any heat treatment requirements for both pipe and end cap. Our engineering team can help you verify this—just reach out when you’re placing an order.
Next, surface preparation. This is the step I see teams rushing through more than any other, and it’s critical for a strong weld. Think of your weld as a bridge between the pipe and end cap; if either side has rust, oil, paint, or mill scale, that bridge has gaps. Before you even pick up a welding torch, you need to clean the 1 to 2 inch area around the end of the pipe that will meet the end cap. For carbon steel, that means grinding away rust and mill scale until you see bright, bare metal. For stainless steel, you have to be extra careful—avoid using carbon steel brushes or grinding wheels, as they can leave iron deposits that cause corrosion in the weld. We always recommend stainless steel-specific abrasives for these jobs.
It’s not just about cleaning, though—you also need to make sure the fit is perfect. The end cap’s bore (the hole that fits over the pipe) should match the pipe’s outer diameter (OD) within a tolerance of 0.005 to 0.010 inches. If the gap between the pipe and end cap is too big, your weld will have extra filler metal that can create weak spots. If it’s too small, you’ll have to force the end cap on, which can distort the pipe or the end cap itself, leading to stress concentrations that cause cracking. Our end caps are precision-machined to meet ANSI B16.9 standards for fit, so you don’t have to worry about sizing issues when you order from us. But you still need to deburr the end of the pipe before fitting the end cap—burrs can create uneven gaps and make alignment hard.
Once the fit and prep are done, the alignment step is where attention to detail matters. Even the slightest misalignment—off-center by more than 1/8 inch—can cause uneven weld penetration. That’s because when you weld, the heat has to be consistent around the joint. If one side is closer to the torch, it will melt faster, leading to thin spots or incomplete fusion. To align properly, use a welding fixture or a level to make sure the end cap is perfectly centered on the pipe. Tacking is another key part here—you should do at least three tack welds around the circumference of the joint, spaced 120 degrees apart. These tacks hold the end cap in place while you do the full weld, and they should be small enough that they don’t create excess heat, but strong enough not to break during the weld. We’ve had clients skip tack welds before, and in one case, the end cap shifted during the full weld, leading to a 2-foot gap that required rework. Don’t cut corners here.
Now, the welding process itself. This is where you have to match your method to the materials you’re working with. For most carbon steel pipes, shielded metal arc welding (SMAW, or stick welding) works well, but for thin-wall pipes or stainless steel, gas metal arc welding (GMAW, or MIG) is better because it gives more precise heat control. The biggest mistake I see here is using too much heat. Excessive heat can cause the weld zone to harden too quickly, or even warp the pipe and end cap. Warping is a big deal because it can throw the joint out of alignment after welding, leading to leaks down the line. That’s why our end caps are designed with uniform thickness—they distribute heat evenly, but you still have to control your torch speed and amperage.
The rule of thumb for weld penetration is 100% fusion—meaning the weld metal has to melt both the pipe and the end cap, not just sit on top of them. You can check this after welding by doing a visual inspection first: look for a smooth, uniform bead around the entire joint, no gaps or undercuts (those are small grooves in the weld that can trap fluid or gas). If you’re working on a high-pressure line, you should also do a non-destructive test, like an ultrasonic test or a hydrostatic test, to make sure there are no hidden flaws. Our technical team can recommend the right test method for your application, depending on whether you’re working in plumbing, oil and gas, or industrial process piping.
Heat treatment is another step that’s often overlooked, especially for high-stress applications like underground pipelines or pressure vessels. When you weld, the heat can create a brittle zone in the base metal right next to the weld, called the heat-affected zone (HAZ). For carbon steel with a carbon equivalent above 0.4%, you need to do post-weld heat treatment (PWHT) to reduce brittleness and relieve stress. This usually involves heating the weld joint to a specific temperature (around 1,100 to 1,200 degrees Fahrenheit) and holding it there for a set time, then cooling it slowly. For stainless steel, you might need to do a passivation treatment after welding to remove any chromium carbide that forms in the HAZ, which can make the steel prone to corrosion. Our end caps are made from materials that respond well to standard heat treatments, so just follow the guidelines for your pipe material, and you’ll be good.
Let me also talk about common mistakes specific to weld end caps, since that’s what we supply. A lot of people think end caps are just flat plates, but no—our weld end caps have a transition zone between the bore and the end plate that’s engineered to distribute stress evenly around the pipe. If you weld too close to the edge of the end cap’s plate, you can miss this transition zone and create a stress riser that will crack over time. We always include a dimensional drawing with every end cap order that marks the safe weld zone, so refer to that. Also, don’t use the end cap as a clamp—some teams try to squeeze the pipe and end cap in a vise to make the fit tighter, but that can distort the end cap’s bore, leading to alignment issues. We precision-machine our end caps to be the exact OD of your pipe, so clamping isn’t necessary if you do your surface prep right.
I want to share a recent success story to put this all together. A water treatment plant client came to us last year with a problem: their end caps were failing on their influent pipes, which carry sediment-laden water. They’d been using a generic end cap and just grinding the pipe end briefly before welding. We supplied them with A53 carbon steel end caps matched to their pipe, and walked their team through the full prep and welding steps: cleaning the pipe with a wire wheel, aligning the end cap with a fixture, doing four tack welds, and using SMAW with controlled amperage. Six months later, they called to say not a single weld had failed, and their maintenance time for those pipes had dropped by 75%. That’s exactly what we’re here for—our end caps aren’t just a product, they’re part of a system that works when you do the steps right.
Now, let’s wrap this up with a quick checklist you can use every time: 1. Confirm material compatibility with your pipe, including grade and heat treatment needs; 2. Clean the pipe end and end cap bore completely, using the right abrasives for your material; 3. Check the fit, making sure the gap between pipe and end cap is within tolerance, and deburr the pipe end; 4. Align the end cap perfectly, using a fixture to avoid off-center welding; 5. Do at least three tack welds around the joint; 6. Control your welding heat to ensure full penetration, no warping, and a uniform bead; 7. Do a visual inspection and, for high-stress applications, non-destructive testing; 8. Apply post-weld heat treatment or passivation as needed.
If you’re working on a project now and want to make sure your end cap welds are as strong as they can be, or if you have questions about material matching for your specific application, don’t hesitate to reach out to our team for a consultation. We’ve worked with every type of piping system—from residential plumbing to offshore oil rigs—and we’re happy to help you pick the right end cap and walk through the process to ensure a solid, long-lasting weld.
Tank Heads References
- American National Standards Institute (ANSI). 2021. ANSI B16.9: Factory-Made Wrought Steel Butt-welding Fittings.
- Welding Research Council (WRC). 2018. Guidelines for Materials Compatibility in Piping Weld Joints.
- American Society of Mechanical Engineers (ASME). 2020. Boiler and Pressure Vessel Code, Section IX: Welding Qualifications.
- International Organization for Standardization (ISO). 2019. ISO 15609: Specification and Qualification of Welding Procedures for Metallic Materials.
Cangzhou Changhui Head Manufacturing Co., Ltd.
We are one of the most professional weld end caps manufacturers and suppliers in China, featured by quality products and good price. Please rest assured to wholesale durable weld end caps for sale here from our factory. Welcome to view our website for more information.
Address: South Industrial Zone, Yanshan County, Cangzhou City, Hebei Province, China.
E-mail: chunle.zhang@changhuitankhead.com
WebSite: https://www.changhuitankhead.com/
